1
00:00:06,060 –> 00:00:11,810
The Concise RDWorks Learning Lab with Russ Sadler.
2
00:00:11,810 –> 00:00:25,540
Session 36 Cutting Thin Materials. Well, in previous sessions, we dealt with the basic principles of cutting. As I explained,
3
00:00:25,540 –> 00:00:32,910
then, there is some, there are some very serious difficulties associated with cutting quite a lot of understanding.
4
00:00:32,910 –> 00:00:37,170
You can just cut stuff without any problem at all. You can make it fall out.
5
00:00:37,170 –> 00:00:48,530
But is it neat? Is it tidy? Is it efficient? Those are the sorts of things, the skills that you’ve got to really start practicing and learning.
6
00:00:48,530 –> 00:00:54,450
Now I can never teach you those skills. I can only show you the principles.
7
00:00:54,450 –> 00:01:01,950
And today we’re going to start off with the easy end of the cutting spectrum, very thin material.
8
00:01:01,950 –> 00:01:06,270
In fact, not only thin material, but very flimsy and weak material.
9
00:01:06,270 –> 00:01:13,690
We’re going to deal with paper and card. What can be difficult about that?
10
00:01:13,690 –> 00:01:18,760
Okay, look, we’ve got some it’s a slightly thicker than inkjet printer paper.
11
00:01:18,760 –> 00:01:27,460
It’s about 110 grams this. So yeah, it stays fairly level and I can support it on these little bars that I’ve got here.
12
00:01:27,460 –> 00:01:32,160
The first thing I’m going to do is find out what the correct focus is for this paper.
13
00:01:32,160 –> 00:01:35,410
Now, if you remember, I’ve got a little automatic test in here,
14
00:01:35,410 –> 00:01:42,730
which because I’ve got a programable z on this machine, allows me to test the focus point at various depths.
15
00:01:42,730 –> 00:01:47,320
So I’ve set it to three millimetre gap under there to start with.
16
00:01:47,320 –> 00:01:52,750
And then we’ll drop the table one millimetre at time and we’ll try and find the correct gap.
17
00:01:52,750 –> 00:02:03,100
For the ideal focus. Now, this is a standard focus test that I’ve got set up on here, and it’s running at cutting speeds of typically 20mm a second,
Transcript for How to Laser Cut Thin Materials (Cont…)
18
00:02:03,100 –> 00:02:22,610
which is not an unreasonable cutting speed and 15 percent power.
19
00:02:22,610 –> 00:02:29,680
Ideally we’re looking for the thinnest line.
20
00:02:29,680 –> 00:02:33,190
Now, remember, I said, I set this to roughly three millimetres to start with,
21
00:02:33,190 –> 00:02:50,810
so that’s three four five six seven eight nine mm, looks to be about the ideal gap that we have for the thinnest possible cutting line. ow 20mm
22
00:02:50,810 –> 00:02:57,190
a second is pretty slow, so we want to find out how quickly and efficiently we can cut this paper.
23
00:02:57,190 –> 00:03:02,770
So if you remember the basic rules that I described to you in the previous session, maximum power.
24
00:03:02,770 –> 00:03:09,500
We’re going to do some test squares because that’s the quickest and the easiest way to try and find out our cutting parameters.
25
00:03:09,500 –> 00:03:14,190
But our first test will be twenty five millimetres a second at
26
00:03:14,190 –> 00:03:25,240
Ninety five percent power, full power basically. It’s done a reasonable job, it’s cut it out,
27
00:03:25,240 –> 00:03:33,340
but it’s also done a lot of scorching around the outside. And look what the heat has done, it has caused distortion on the edge of the paper.
28
00:03:33,340 –> 00:03:36,760
Such a thin material. We should be able to rip through this very quickly.
29
00:03:36,760 –> 00:03:44,890
So let’s put the speed up to one hundred. OHOH. So in case you didn’t see that look.
30
00:03:44,890 –> 00:03:52,360
Several things seem to have happened here. We’ve got terrible reflection off of something.
31
00:03:52,360 –> 00:03:57,460
I think it must be off the back of our grid.
Transcript for How to Laser Cut Thin Materials (Cont…)
32
00:03:57,460 –> 00:04:07,030
So let’s move my supports out the way and we’ll do the same thing again. A-ha!
33
00:04:07,030 –> 00:04:11,350
So now it’s clean and we don’t have any burn marks.
34
00:04:11,350 –> 00:04:14,800
So it just shows you, doesn’t it? What
35
00:04:14,800 –> 00:04:22,930
reflection off of things can do for your cuts, especially on thin materials like this, which are very sensitive.
36
00:04:22,930 –> 00:04:33,970
Now there is some browning around the edge here if we look. It’s not exactly perfectly clean and is that on the back or the front?
37
00:04:33,970 –> 00:04:42,400
Well, the front looks reasonably clean when we look around here, and so does the back.
38
00:04:42,400 –> 00:04:50,080
Although there is just a hint there on the back of some sort of scorch mark just there.
39
00:04:50,080 –> 00:04:59,170
So maybe high power and high speed is not the right approach for paper.
40
00:04:59,170 –> 00:05:11,530
I can turn my air assist on or I can regulate it back with this ball valve to just the merest whisper to protect the lens from getting smoked up.
41
00:05:11,530 –> 00:05:17,200
You can hear how silent things are at the moment, except for that small amount of air that you can hear in the background.
42
00:05:17,200 –> 00:05:27,010
Let me turn that down a little bit more. There we go. Now you can hardly hear any air at all.
43
00:05:27,010 –> 00:05:35,200
So let’s just run that cut again. The cut is absolutely silent.
44
00:05:35,200 –> 00:05:40,240
It just dropped out. I’m going to change the settings on this machine.
45
00:05:40,240 –> 00:05:44,840
We’re still going to leave it at 100mm a second.
46
00:05:44,840 –> 00:05:54,220
And now listen very carefully and compare what you hear this time with what you heard last time.
47
00:05:54,220 –> 00:05:58,660
Can you hear that noise? Listen again. It’s no longer silent.
Transcript for How to Laser Cut Thin Materials (Cont…)
48
00:05:58,660 –> 00:06:10,090
It’s what I like to call hissy. Listen and hear what I mean.
49
00:06:10,090 –> 00:06:16,310
Did you hear it? Now, I’m still using 100mm a second.
50
00:06:16,310 –> 00:06:23,120
But I’m only using 15 percent power. I’m probably down at something like about 20 watts.
51
00:06:23,120 –> 00:06:41,550
And if we take a look at my ammeter while I’m running that cut. We’ll notice that it probably only goes up to maybe four, six, five milliamps. Four milliamps.
52
00:06:41,550 –> 00:06:45,290
I mean, that’s half of nothing. So what’s going on?
53
00:06:45,290 –> 00:06:53,720
The quality of the cut is superb. There’s no smoke marks or damage to it, either on the top or the underneath.
54
00:06:53,720 –> 00:06:59,900
How am I able to get such a clean cut at such a low power and such a high speed?
55
00:06:59,900 –> 00:07:05,150
This is a calibration graph for typically this sort of machine.
56
00:07:05,150 –> 00:07:10,010
And what we’ve got here is 0 to 100 percent power.
57
00:07:10,010 –> 00:07:16,580
And up here, we’ve got 0 to 90 watts and this happens to be in this machine, about an 80 watt tube.
58
00:07:16,580 –> 00:07:25,970
And what happens is when you select zero to 100 percent power, you’re actually selecting milliamps, the current that flows through the tube.
59
00:07:25,970 –> 00:07:33,080
You’re not actually selecting watts. The Watts are related to the milliamps in a very non-linear way.
60
00:07:33,080 –> 00:07:42,350
It’s all to do with the physics, but it’s not linear. And as you can see here, we get the power coming up in a strange, non-linear fashion.
61
00:07:42,350 –> 00:07:51,860
And so consequently, we’ve got an 80 watt tube. You might think that 25 percent a quarter of 80 watts would be roughly 20 watts.
62
00:07:51,860 –> 00:08:01,460
Well, look, here is 25 percent. Power takes us up here to nearly 50 watts, so that’s nowhere near what you might expect.
Transcript for How to Laser Cut Thin Materials (Cont…)
63
00:08:01,460 –> 00:08:07,640
And 50 percent power 40 watts. Well, 50 percent power is up here, nearly 70 watts.
64
00:08:07,640 –> 00:08:14,300
So there is totally no sense in looking at watts in terms of percent power.
65
00:08:14,300 –> 00:08:21,620
You have to understand how your machine works because this scale is not related to Watts, and I can’t stress that enough.
66
00:08:21,620 –> 00:08:26,900
If we look at this red graph, you’ll see that it drops down to here and stops.
67
00:08:26,900 –> 00:08:36,950
This might not be exactly the right number that I’ve drawn on this graph, but somewhere down here below, these are millliamps remember, as well.
68
00:08:36,950 –> 00:08:42,680
And we’ve just seen that at 4 milliamps, we’re getting tremendous power out of this machine.
69
00:08:42,680 –> 00:08:46,040
We were able to cut the paper at 100 millimeters a second.
70
00:08:46,040 –> 00:08:51,560
That that just doesn’t make sense because this graph says that there’s virtually no power down here at all.
71
00:08:51,560 –> 00:08:56,300
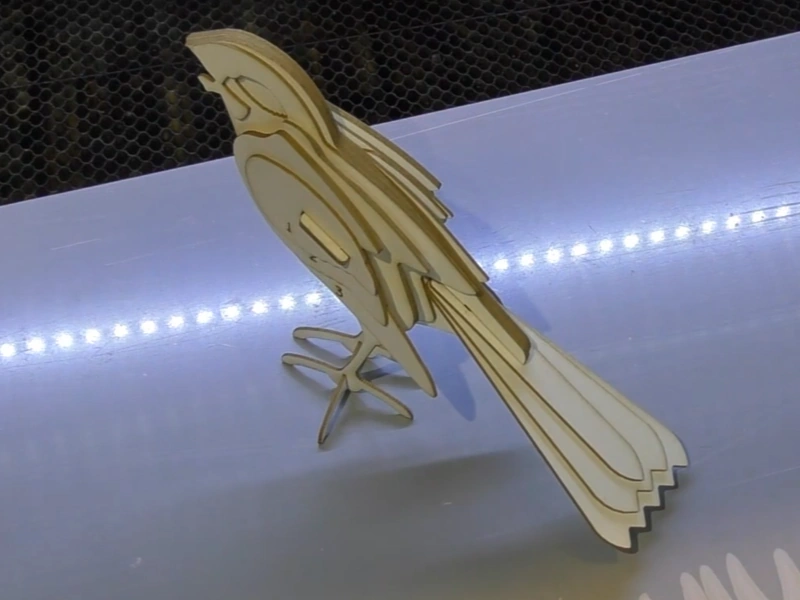
What is going on now? The laser tube is something called a gas discharge tube.
72
00:08:56,300 –> 00:09:02,000
If you’re very old like me, you remember them as valves in radio, in steam radio.
73
00:09:02,000 –> 00:09:08,390
If you’re younger, you still know what a gas discharge tube is, even if you don’t know.
74
00:09:08,390 –> 00:09:18,460
I’ll show you that you do know. OK, now hiding under one of my cabinets here in my workshop we’ve got one of these things it’s a fluorescent tube.
75
00:09:18,460 –> 00:09:25,890
This is a gas discharge tube. And it’s quite an old tube now, and it takes a little bit of time to kick into action.
76
00:09:25,890 –> 00:09:37,120
Let me just show you. So there we go, Look, it’s glowing at this end here and then all of a sudden “Ping” it jumps into life now that glow at the end there.
77
00:09:37,120 –> 00:09:47,320
Is something called a ray discharge? It took a little bit of time for that beam to come on completely.
78
00:09:47,320 –> 00:09:54,190
The same mechanism operates in our gas discharge tube, the laser tube.
79
00:09:54,190 –> 00:10:00,020
So we’re just going to set up a little demonstration to show you the relationship between this missing bit
Transcript for How to Laser Cut Thin Materials (Cont…)
80
00:10:00,020 –> 00:10:06,910
of data or this very strange bit of information at the bottom here and the fluorescent tube starter that you’ve just seen.
81
00:10:06,910 –> 00:10:10,450
I’ve found a very useful job for my cup of coffee.
82
00:10:10,450 –> 00:10:16,240
I’m going to run this machine and I’m going to fire the laser beam into my cup of coffee, but for safety reasons,
83
00:10:16,240 –> 00:10:25,160
because firing it down into that coffee, all the energy will be absorbed into my cup.
84
00:10:25,160 –> 00:10:30,080
So that’s all it’s going to do. OK, so I’ve set the power now to eight percent.
85
00:10:30,080 –> 00:10:33,980
Technically, that’s almost off the scale, and maybe we shall find that
86
00:10:33,980 –> 00:10:43,580
we’ve got zero cutting ability. But we can just check that, we’ll just run that program onto my piece of paper there.
87
00:10:43,580 –> 00:10:49,400
My cup is underneath remember. It’s just about scorching the paper.
88
00:10:49,400 –> 00:10:55,190
If we look, it’s certainly not cutting through the paper.
89
00:10:55,190 –> 00:11:01,190
So as near as, damn it, zero power, so this is the output end of the tube.
90
00:11:01,190 –> 00:11:09,590
And what we’re going to do, we’re going to study what’s happening just here at the cathode.
91
00:11:09,590 –> 00:11:17,240
Remember, the fluorescent tube? The end of the tube was the bit that lit up first before the whole of the tube illuminated.
92
00:11:17,240 –> 00:11:22,070
And look, can you see the merest little glow in here?
93
00:11:22,070 –> 00:11:27,290
So I’m now going to change that to 10 per cent. We’re going to go up in two per cent power steps.
94
00:11:27,290 –> 00:11:34,520
Now you can see it’s a lot brighter. That length, of the glow has got a little bit longer.
95
00:11:34,520 –> 00:11:41,360
Now we’re at 12 percent. The glow is traveling further along the tube.
96
00:11:41,360 –> 00:11:48,620
It’s not all the way along the tube, but you’ll notice how unstable that glow is.
97
00:11:48,620 –> 00:11:59,930
Now we’ll go to 14. Now we can see the glow is beginning to creep along the tube a bit more.
Transcript for How to Laser Cut Thin Materials (Cont…)
98
00:11:59,930 –> 00:12:08,130
It’s certainly not all the way along. Now we go to 16 per cent.
99
00:12:08,130 –> 00:12:13,590
It’s still not a really powerful beam, but it’s getting brighter just here, as you can see.
100
00:12:13,590 –> 00:12:18,030
And it is beginning to go along the tube a bit.
101
00:12:18,030 –> 00:12:24,720
Let’s just stop there and you watch when the tube goes out, it’s very, very faint and then it disappears.
102
00:12:24,720 –> 00:12:29,820
But the whole thing is that this tube, this beam is continuously fluttering.
103
00:12:29,820 –> 00:12:43,700
If you look, it’s misty. It’s very random in its motion and 22 percent.
104
00:12:43,700 –> 00:12:51,380
Well the beam is starting to travel along the tube now, but look how fluttery and unstable that beam is.
105
00:12:51,380 –> 00:12:58,310
It’s nearly along the whole length of the tube now. And this is 24 percent.
106
00:12:58,310 –> 00:13:07,070
This is 26 percent. No, we’ve still got lots of instability in the beam, even at 26 percent. Now look at 28 percent.
107
00:13:07,070 –> 00:13:14,510
That beam is completely stable, but the current is still only four milliamps.
108
00:13:14,510 –> 00:13:18,590
So lets go up to 30 per cent. It’s a pretty stable beam.
109
00:13:18,590 –> 00:13:26,370
You can hear my cup of coffee crackling away in the front of the machine as the power increases.
110
00:13:26,370 –> 00:13:32,270
We’re at 30 percent at the moment, and I’m going to drop this down to say 24 percent.
111
00:13:32,270 –> 00:13:41,030
And you can definitely see the fluttery nature of the beam, the difference between 24 percent and 30 percent.
112
00:13:41,030 –> 00:13:47,810
OK, now that’s the difference between pre ionization and full ionization.
113
00:13:47,810 –> 00:13:52,700
This current control is managed by the high voltage power supply.
114
00:13:52,700 –> 00:13:57,220
But as you saw with that beam, it was very flaky, it was very misty.
Transcript for How to Laser Cut Thin Materials (Cont…)
115
00:13:57,220 –> 00:14:03,230
It was very wispy. The current flow was effectively out of control.
116
00:14:03,230 –> 00:14:12,200
And what was actually happening there? We were getting little bursts of current there, very high bursts of current for maybe a few nanoseconds.
117
00:14:12,200 –> 00:14:19,640
So effectively, we may well have more power down here than we have up here.
118
00:14:19,640 –> 00:14:30,320
But this is stable power and down here, it’s incredibly high and totally random frequency and amount of power.
119
00:14:30,320 –> 00:14:38,600
So we’ve got this very weird power zone down at the bottom here.
120
00:14:38,600 –> 00:14:45,140
And because, as I said, it’s very, very high power. When we get weak material, thin, weak material like paper,
121
00:14:45,140 –> 00:14:56,930
these very high power pulses are able to burst through our paper and do damage without any burning. It just instantly evaporates
122
00:14:56,930 –> 00:15:06,200
the paper and the carbon. Now it doesn’t work when you’re starting to do things like thick or three millimetre thick, acrylic or 3mm thick.
123
00:15:06,200 –> 00:15:12,320
And the way that you can tell is you can hear this hissy mode and the hissy mode is,
124
00:15:12,320 –> 00:15:18,110
in fact, this very high frequency, pulsing hitting the paper and causing damage.
125
00:15:18,110 –> 00:15:20,990
As I say, cutting is quite a complex process.
126
00:15:20,990 –> 00:15:29,420
And this pre ionization zone is also the zone that we tend to use for things like photo engraving, which I’ve probably mentioned before.
127
00:15:29,420 –> 00:15:33,080
This pulsing mode is a very powerful mode. So really,
128
00:15:33,080 –> 00:15:39,980
what you need to do is work out on your tube, identify between what percentage and what percentage
129
00:15:39,980 –> 00:15:46,580
you get this pre ionization and then use towards the top end of the zone that you identify.
130
00:15:46,580 –> 00:15:53,300
We’ve identified 30 as being stable and 25 is definitely being hissy.
131
00:15:53,300 –> 00:15:59,810
And that’s where I would tend to set the optimum cutting if I wanted to do paper or card.
Transcript for How to Laser Cut Thin Materials (Cont…)
132
00:15:59,810 –> 00:16:05,600
So here I’ve got some white card. This is really about probably half millimetre thick,
133
00:16:05,600 –> 00:16:18,290
and the reason why it’s shiny and smooth is because it’s got a lot of Kaolin or China cray built into the paper that makes it stiff and smooth.
134
00:16:18,290 –> 00:16:23,570
Now, China clay is a mineral material which doesn’t burn,
135
00:16:23,570 –> 00:16:30,720
and this does not have the same burn properties as that paper that you just saw. We’re already set to 30 percent.
136
00:16:30,720 –> 00:16:37,340
We’ll just run a test square. And we’ve done that at 100 mm a second.
137
00:16:37,340 –> 00:16:43,610
And it’s a thick up paper. And so consequently, it might not drop out.
138
00:16:43,610 –> 00:16:48,260
I think you can see how smoky it is around the cuts.
139
00:16:48,260 –> 00:16:51,650
As you can see, 30 percent power hasn’t really cut out.
140
00:16:51,650 –> 00:16:59,750
It’s got those Ferrari effects that I was telling you about look dark in the corner, but missing along the center.
141
00:16:59,750 –> 00:17:10,280
So we’re going to leave the head at exactly the same position. And all I’m going to do now is to change the power from 30 down to 24, lower power
142
00:17:10,280 –> 00:17:14,480
technically. It didn’t cut at 30, remember?
143
00:17:14,480 –> 00:17:19,940
So what’s it going to do at 24, it must by default cut even worse.
144
00:17:19,940 –> 00:17:26,990
So listen and watch.
145
00:17:26,990 –> 00:17:37,010
And sure enough, a little less power means we’ve actually not made it quite as dark in the center of the cut.
146
00:17:37,010 –> 00:17:42,850
But what we have done is probably got a little bit further into the cut.
147
00:17:42,850 –> 00:17:55,540
Away from the corners, we’ve now dropped the speed from 100 to 80, very noisy, and that is hanging in by the merest thread.
148
00:17:55,540 –> 00:18:02,230
So we drop the speed to 70. And there we go.
Transcript for How to Laser Cut Thin Materials (Cont…)
149
00:18:02,230 –> 00:18:10,780
It drops out completely, OK? On each of the corners where the beam runs away from the corner, it’s leaving a little trail behind it.
150
00:18:10,780 –> 00:18:16,510
That’s the smoking effect of this Kaolin that’s in this card. That’s why I don’t use this card.
151
00:18:16,510 –> 00:18:24,220
I bought this card originally because I thought it was an amazing, lovely piece of material to make Christmas cards or birthday cards with.
152
00:18:24,220 –> 00:18:27,850
No, it’s rubbish at actually cutting,
153
00:18:27,850 –> 00:18:33,490
as you can see. This is a creamy, much softer.
154
00:18:33,490 –> 00:18:37,030
This is not as dressed with Kaolin as the other one.
155
00:18:37,030 –> 00:18:47,230
There may be a very small amount in it, but it’s negligible and this time – the cuts are virtually clean.
156
00:18:47,230 –> 00:18:54,550
Although I use this for cards, what I normally do use it the wrong way round.
157
00:18:54,550 –> 00:18:58,300
In other words, I will reverse my images and cut them from the back.
158
00:18:58,300 –> 00:19:03,670
Now, here’s what I’ve found is one of the best materials for cutting when I do my cards.
159
00:19:03,670 –> 00:19:10,570
It’s a fairly thick 200 gram, but it’s you can see, it’s a watercolour paper and it’s a bit like a very,
160
00:19:10,570 –> 00:19:15,640
very thick cartridge paper that’s probably again half a millimeter thick.
161
00:19:15,640 –> 00:19:28,600
But it’s got none of the sort of additives in it. It’s a beautifully flat piece of paper, cuts without a mark.
162
00:19:28,600 –> 00:19:36,520
And here we are, cutting at 170 millimetres a second.
163
00:19:36,520 –> 00:19:45,850
This is a sort of job that I would do with this setting.
164
00:19:45,850 –> 00:20:02,590
Now, I don’t need to turn my air assist on, but I normally turn it on so that, let’s just stop that, I normally turn it on so that any of the pieces blow away.
Transcript for How to Laser Cut Thin Materials (Cont…)
165
00:20:02,590 –> 00:20:11,650
It’s not for any other reason than just blowing the pieces cleanly out the bottom of the work.
166
00:20:11,650 –> 00:20:23,320
I transferred this file from my other machine.
167
00:20:23,320 –> 00:20:31,480
So it’s totally the wrong way round because the datum on this machine is the opposite corner to the other machine.
168
00:20:31,480 –> 00:20:44,980
But really, this is just a demonstration to show you the sort of thing that you can do with this sort of mode.
169
00:20:44,980 –> 00:20:48,290
So I’m not going to I’m not going to take that through to conclusion,
170
00:20:48,290 –> 00:20:57,380
but that’s just an idea of the sort of stuff you can do. Now that was done at 100 millimetres a second.
171
00:20:57,380 –> 00:21:07,610
Remember, don’t leave debris behind because debris can catch fire, and this time we’ll run it at 200mm a second.
172
00:21:07,610 –> 00:21:09,960
Why would this work at 200mm a second?
173
00:21:09,960 –> 00:21:17,720
Well, remember the Ferrari effect when these dimensions are very small, it will never get up to 200 millimetres a second.
174
00:21:17,720 –> 00:21:22,850
It will only ever get up to 200 millimetres a second on the long, thin strokes,
175
00:21:22,850 –> 00:22:03,780
but it will achieve the fastest possible cutting speeds it can on those small cuts.
Transcript for How to Laser Cut Thin Materials (Cont…)
176
00:22:03,780 –> 00:22:13,660
{hissing sound of laser cutter}.
177
00:22:13,660 –> 00:22:30,360
Large things like this where it’s not going to exceed the damage threshold as I might not be cutting on these very large outer shapes.
178
00:22:30,360 –> 00:22:41,850
Just about, just about, so 200mm a second is really too fast for that job because it’s not too fast for these,
179
00:22:41,850 –> 00:22:47,850
but it’s too fast for these straights if you like where you do get up to 200 miles an hour.
180
00:22:47,850 –> 00:22:51,870
We could reclaim this because it’s basically perforated.
181
00:22:51,870 –> 00:23:01,560
So I hope you can see that although it hasn’t pierced through completely, it’s actually perforated because of the randomness of the high power pulses.
182
00:23:01,560 –> 00:23:10,310
Some of it is perforated through. So that’s how we can actually still,
183
00:23:10,310 –> 00:23:16,460
effectively reclaim that. With the right material and an understanding of what the right settings are.
184
00:23:16,460 –> 00:23:21,590
You can do some really nice work with thin card and thin materials.
185
00:23:21,590 –> 00:23:28,760
Two things first of all. Here I’ve got some white card, which is basically what they use for making beer mats.
186
00:23:28,760 –> 00:23:35,870
It’s a very soft white card, which is basically almost like grainless wood because it is just wood pulp.
187
00:23:35,870 –> 00:23:44,240
There’s no China Clay or anything in this and I often use this for making cardboard models, which is what we’re going to do today.
188
00:23:44,240 –> 00:23:52,580
You will notice that I’ve got this stuff on here that I am not very keen on because it normally marks the back of your product.
189
00:23:52,580 –> 00:24:01,470
There are times, like today, when you can use it with almost zero effect on the back of your product.
Transcript for How to Laser Cut Thin Materials (Cont…)
190
00:24:01,470 –> 00:24:11,540
If you’re using this pre ionization or hissy mode, you will find that it has virtually no effect on the back of the product.
191
00:24:11,540 –> 00:24:20,390
I can be lazy because when you see what I’m going to cut out of this piece of paper, it would take me quite a long time to put all the bridges in.
192
00:24:20,390 –> 00:24:26,360
That would allow me to lift this up, put it on some pins or my strips and prevent the parts from falling out.
193
00:24:26,360 –> 00:24:31,040
Because if parts fall out, then it’s possible that you’ll get burn marks.
194
00:24:31,040 –> 00:24:38,780
If the parts overlap, the next cut. So I’ve got this machine set up and what I’ve done, I’ve put my zero point right on the corner of the paper
195
00:24:38,780 –> 00:24:45,710
there. Now I can check that because all I’ve got to do is go {pulse} and you can see that a little teeny weeny white dot of
196
00:24:45,710 –> 00:24:52,970
light is right in the corner of the paper. That tells me that I’ve got the correct zero or origin starting point.
197
00:24:52,970 –> 00:25:02,390
Now I need to put some extraction on for this. This happens to be a nice flat card.
198
00:25:02,390 –> 00:25:06,950
Sometimes you may well find if you turn it the wrong way, the corners might stick up.
199
00:25:06,950 –> 00:25:12,290
So make sure that the sticky up corners are down.
200
00:25:12,290 –> 00:25:19,310
And then there’s a fair chance that the middle will get pulled down by the vacuum that’s underneath here.
201
00:25:19,310 –> 00:25:30,680
We’ve got most of our air drawing through here. So what we can do, we can improve the suction at this point here by blocking off most of the air.
202
00:25:30,680 –> 00:25:37,580
So now this card is being very gently pulled down by the vacuum.
203
00:25:37,580 –> 00:25:55,400
OK, well, we’re going to turn some air on now. So we’ve got air assist on this because we’re cutting.
Transcript for How to Laser Cut Thin Materials (Cont…)
204
00:25:55,400 –> 00:26:07,370
I’m running this at 35mm/s, but I’m also running at only 25 per cent, which is towards the top end of my pre ionization mode.
205
00:26:07,370 –> 00:26:11,630
If you remember. Even though this is one point one millimetres thick.
206
00:26:11,630 –> 00:26:15,440
We’re running at about four milliamps. This is not a continuous cut.
207
00:26:15,440 –> 00:26:22,580
This is like a perforated cut. You’ve got very high power, for very, very short intervals here,
208
00:26:22,580 –> 00:26:28,850
which means we’re able to do a lot of damage without doing a huge amount of burning to the product.
209
00:26:28,850 –> 00:26:38,660
We’re only just using the central power of the laser beam itself, not the outer intensity, low intensity scorching parts of the beam.
210
00:26:38,660 –> 00:26:43,790
So as you can see, this would be a bit of a challenge.
211
00:26:43,790 –> 00:26:54,710
I’d have to go round and bridge every one of these pieces, but hopefully now if I’ve done this right.
212
00:26:54,710 –> 00:27:01,150
And if we take a look at the back, which is the important bit, just a few odd scorch marks here and there,
213
00:27:01,150 –> 00:27:09,990
but nothing that’s going to cause any real damage to the product, as you can see. Now, these parts are numbered.
214
00:27:09,990 –> 00:27:17,150
I’ve got another sheet I’ve got to cut. We’ll start in the middle at eight, and we put that through there.
215
00:27:17,150 –> 00:27:24,770
And we put seven on the back of six, five and five.
216
00:27:24,770 –> 00:27:28,360
Put that on there like that, and there we’ve got the start of that bird.
217
00:27:28,360 –> 00:27:36,660
And we’ve got the tail. So that’s the beginning of our Model Bird. We’ll just go and make the other parts of the wings.
218
00:27:36,660 –> 00:27:55,090
So we’ve got one,
219
00:27:55,090 –> 00:28:02,690
two and three, which will fit on onto here.
Transcript for How to Laser Cut Thin Materials (Cont…)
220
00:28:02,690 –> 00:28:15,670
So I think that five goes in front of four and I think four fits behind it and just literally pushes in there to lock everything in.
221
00:28:15,670 –> 00:28:23,770
And one and there’s our little model bird, so there’s all sorts of things you can do with this machine.
222
00:28:23,770 –> 00:28:27,130
This was originally designed for two or three millimeter thick material,
223
00:28:27,130 –> 00:28:31,570
so I had to, I’ve had to go round and modify all the slots and grooves to make things fit.
224
00:28:31,570 –> 00:28:35,740
This is quite thick card at one millimetre thick, or 1.1 millimetre thick.
225
00:28:35,740 –> 00:28:40,630
And I’m still catching it with pre ionization power.
226
00:28:40,630 –> 00:28:45,770
Now I will explain in the next session why I’ve done this little demonstration
227
00:28:45,770 –> 00:28:53,290
with card, and why we started off with the easy jobs cutting thin paper and card.
Transcript for How to Laser Cut Thin Materials
 Skip to content